Kinservo
Robot workstations机器人工作站
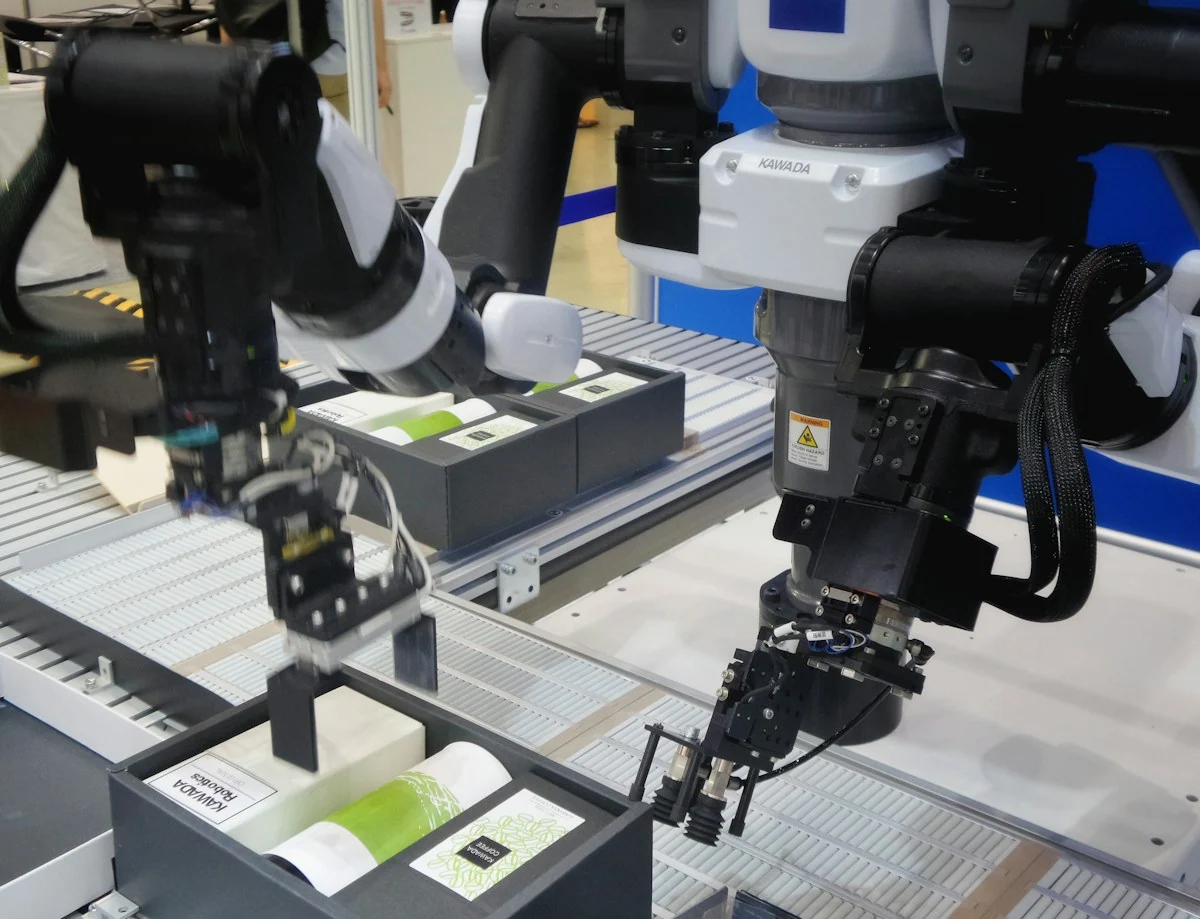
Machine tending, assembly and palletizing with part-specific tooling and safeguarding.适用于机床上下料、装配和码垛,按工件设计夹具与防护。
View solution查看方案 Kinservo
Coordinate equipment signals and production records between PLCs, inspection stations and site systems.梳理 PLC、检测工位和工厂系统之间的设备信号与生产记录。
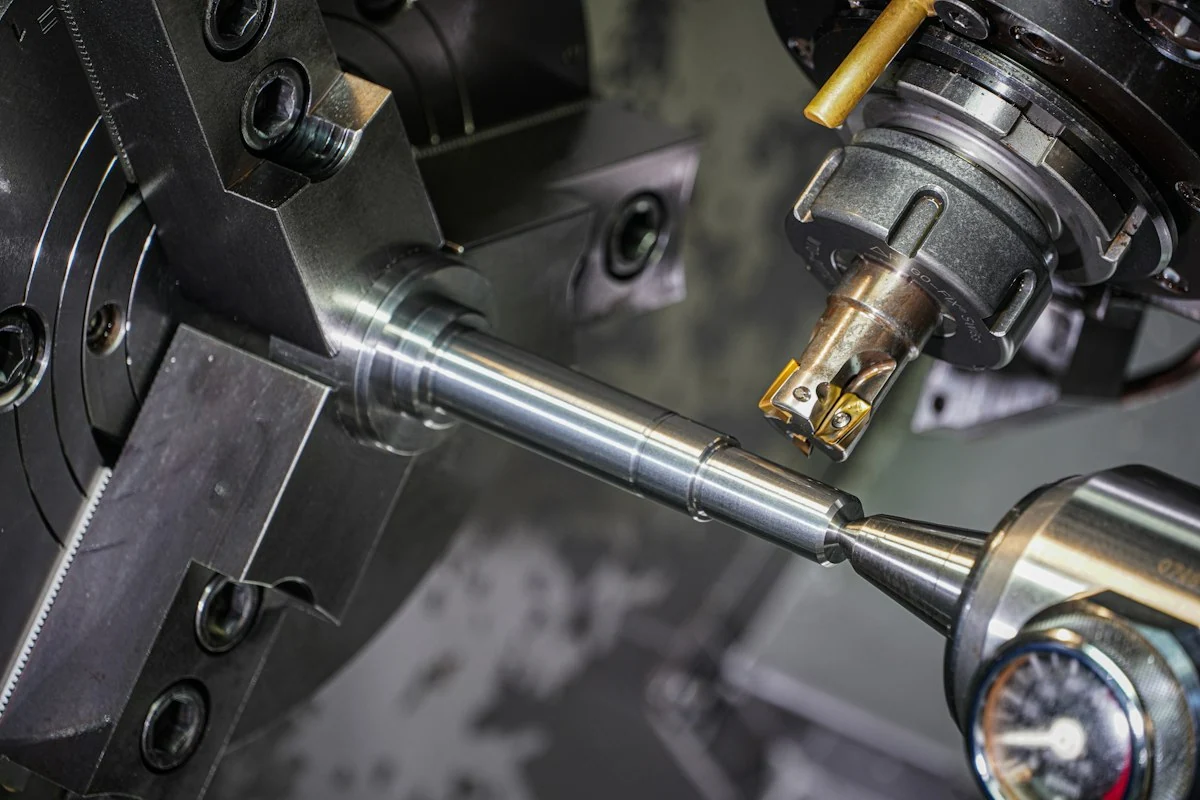
Design around the part datum, tolerance and access for inspection and maintenance.围绕工件基准、公差及检测与维护空间设计工装。
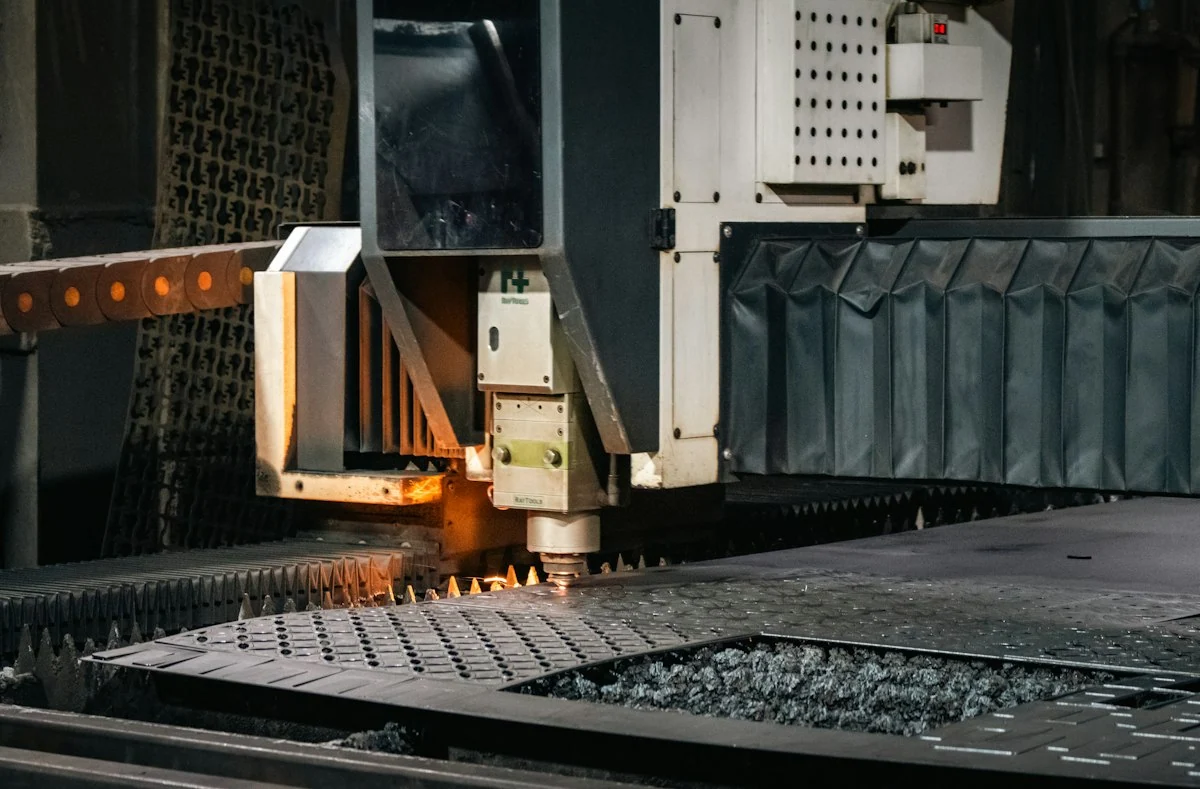
Review interchange points between feeding, processing and inspection modules when planning capacity changes.规划产量变化时,预留供料、加工和检测模块之间的交接条件。
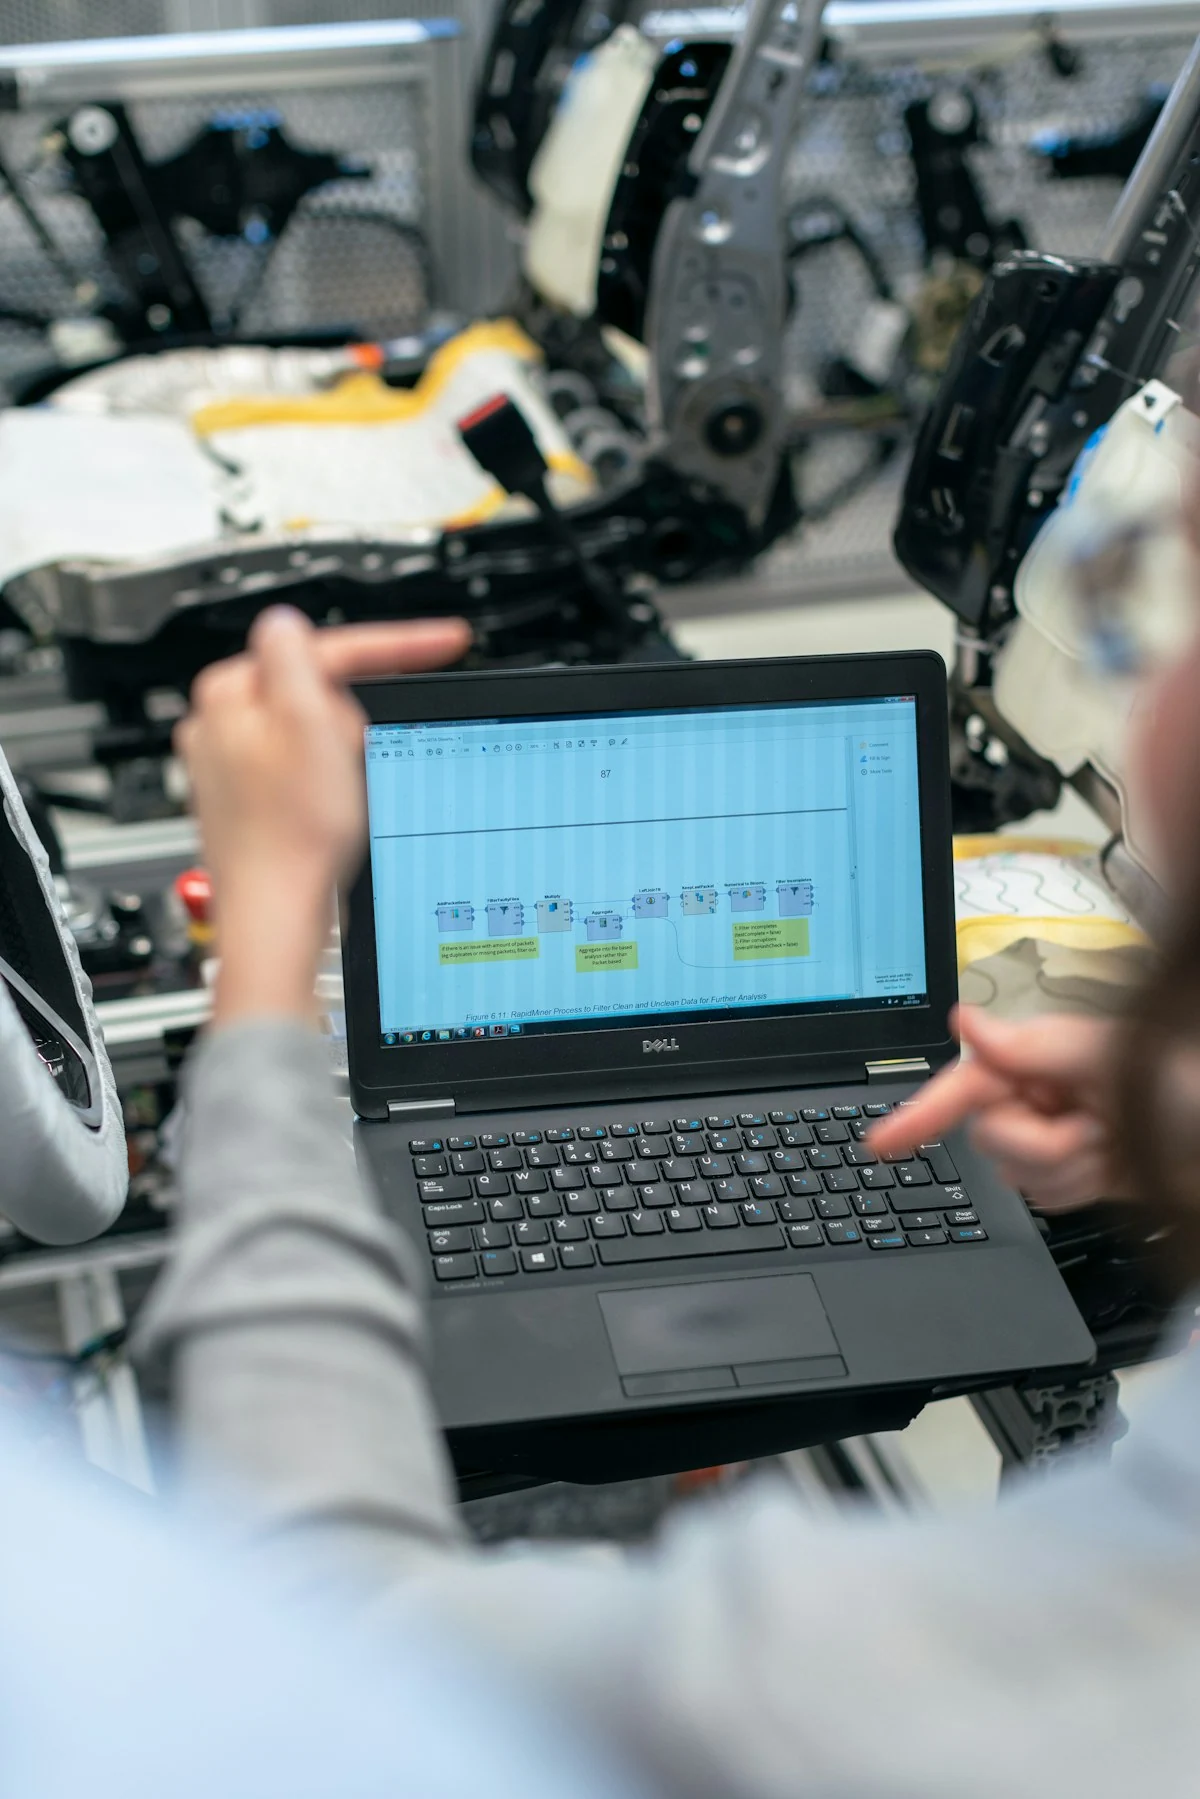
Plan training, parts, backups and maintenance access around the approved equipment configuration.根据确认的设备配置规划培训、易损件、程序备份和维修空间。
Machine tending, assembly and palletizing with part-specific tooling and safeguarding.适用于机床上下料、装配和码垛,按工件设计夹具与防护。
View solution查看方案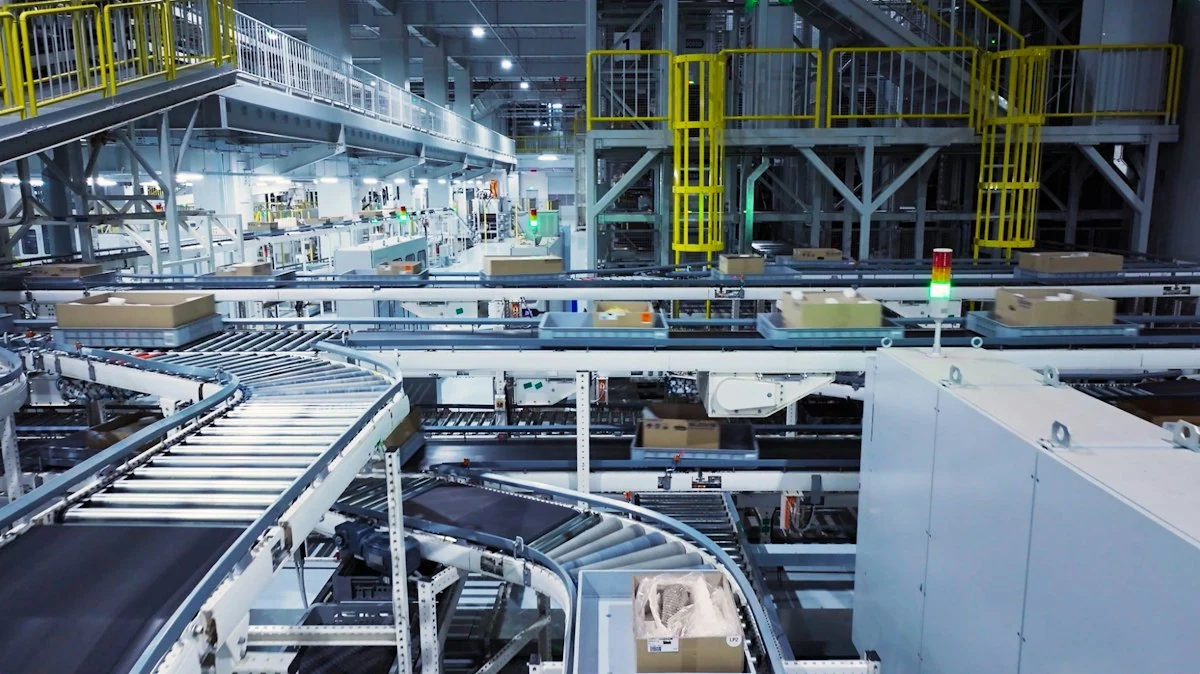
Infeed, accumulation, identification and diversion for cartons and totes.面向纸箱、周转箱的供料、缓存、识别与分流。
View solution查看方案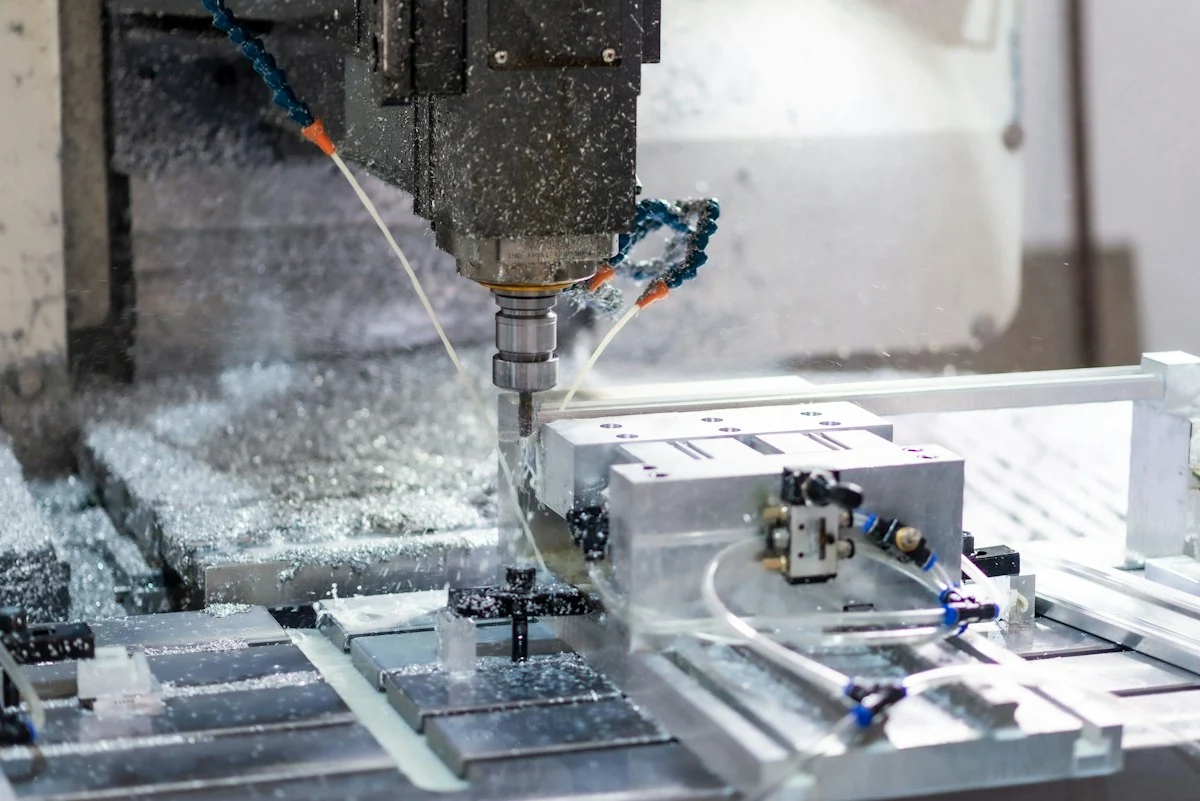
CNC equipment with automated loading, workholding and gauging.将数控机床、自动上下料、工装及测量组合成加工单元。
View solution查看方案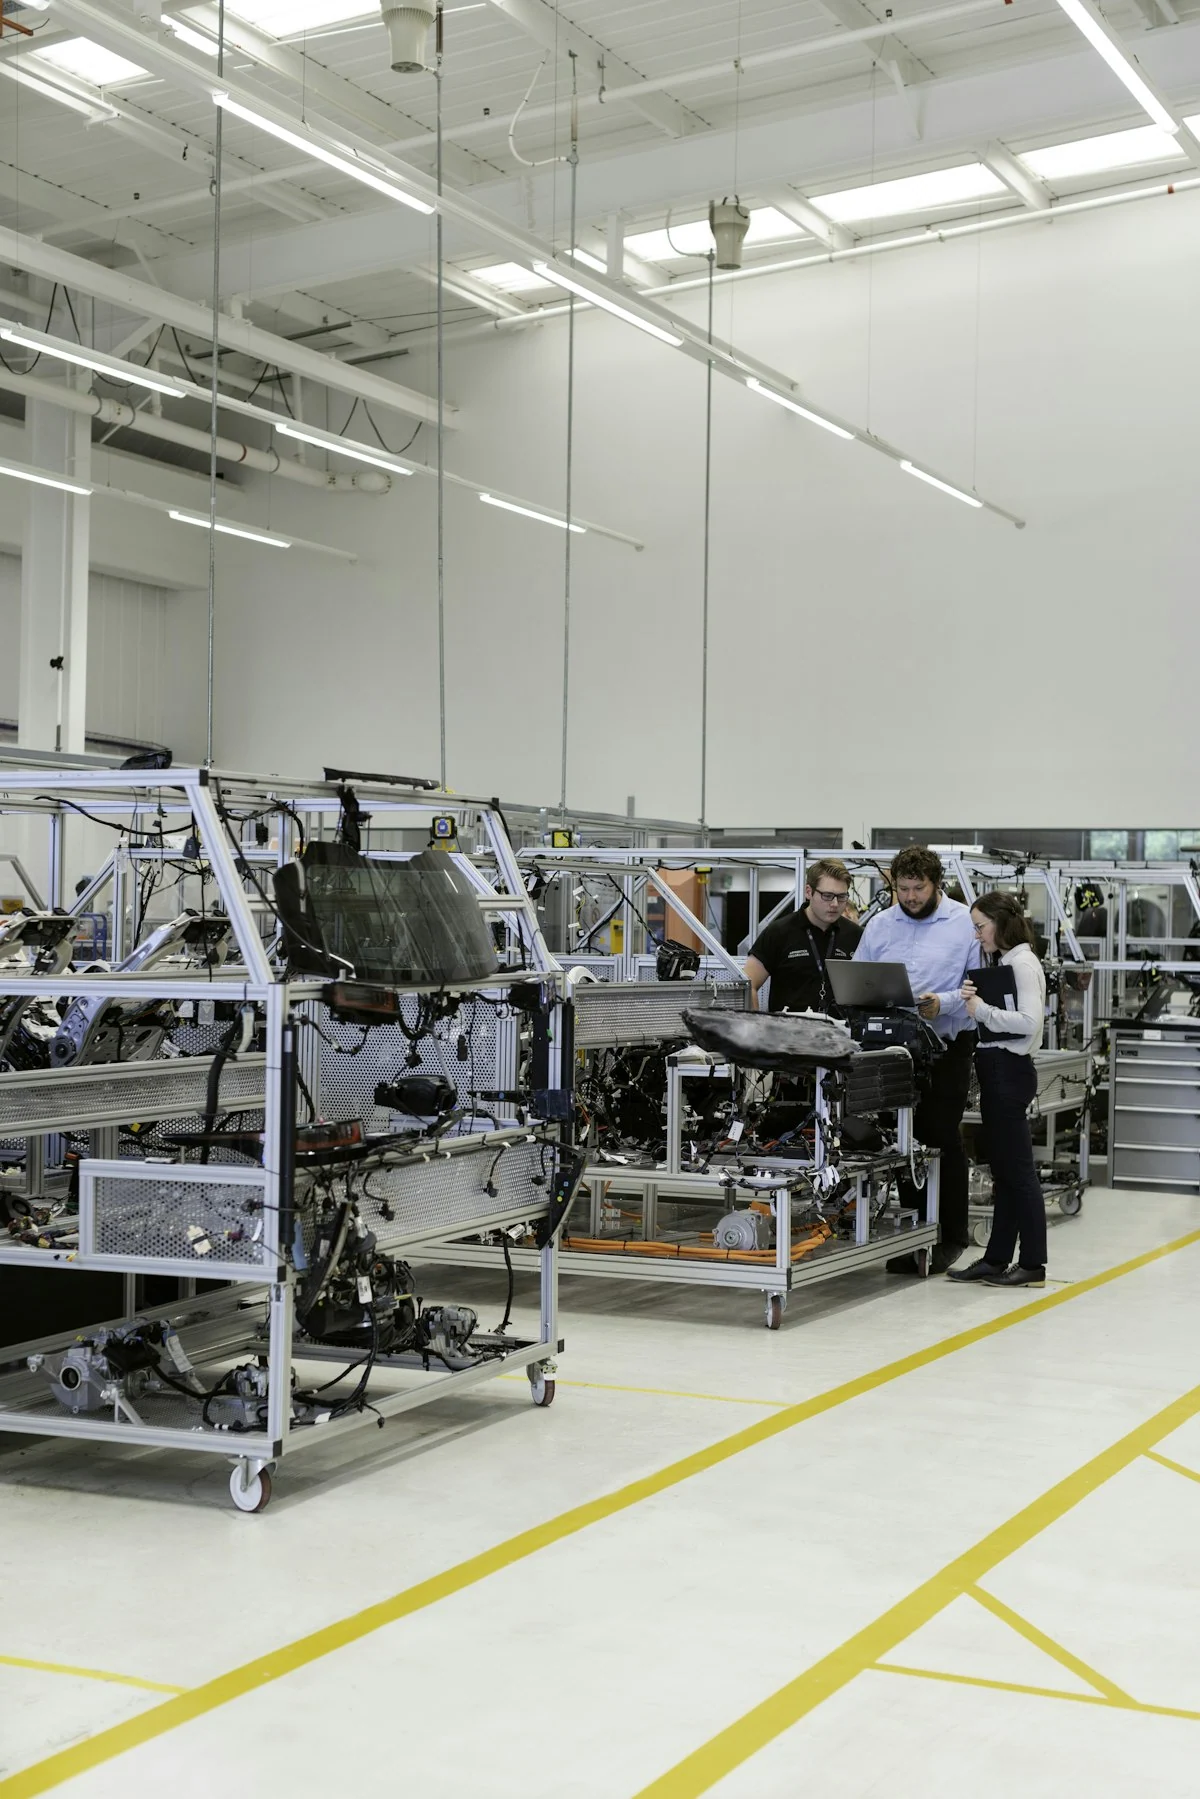
Measure real cycle times and map site constraints before setting targets.实测节拍并梳理现场约束,明确工程目标。
View this phase查看该阶段
Review the layout, safety concept, control interfaces and test plan.评审布局、安全设计、控制接口和测试计划。
View this phase查看该阶段
Test with production parts, verify site interfaces and hand over documentation.使用生产工件试运行,验证现场接口并移交资料。
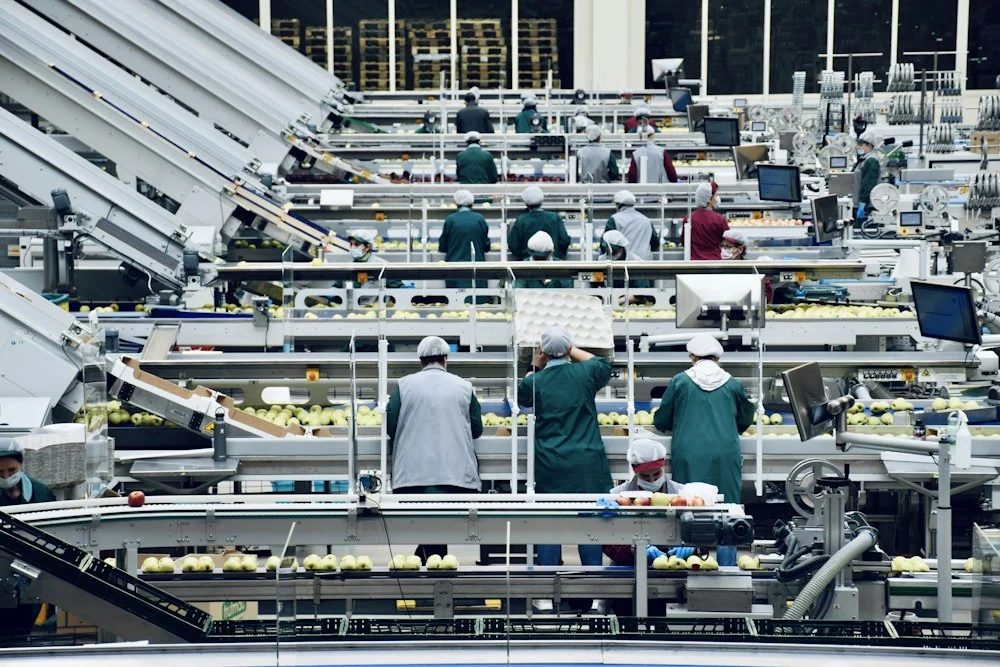
View this phase查看该阶段How many cartons must the line handle in the busiest hour, and what happens when a sorting lane fills up?高峰一小时要处理多少箱?分流口满位后,产线如何处理?
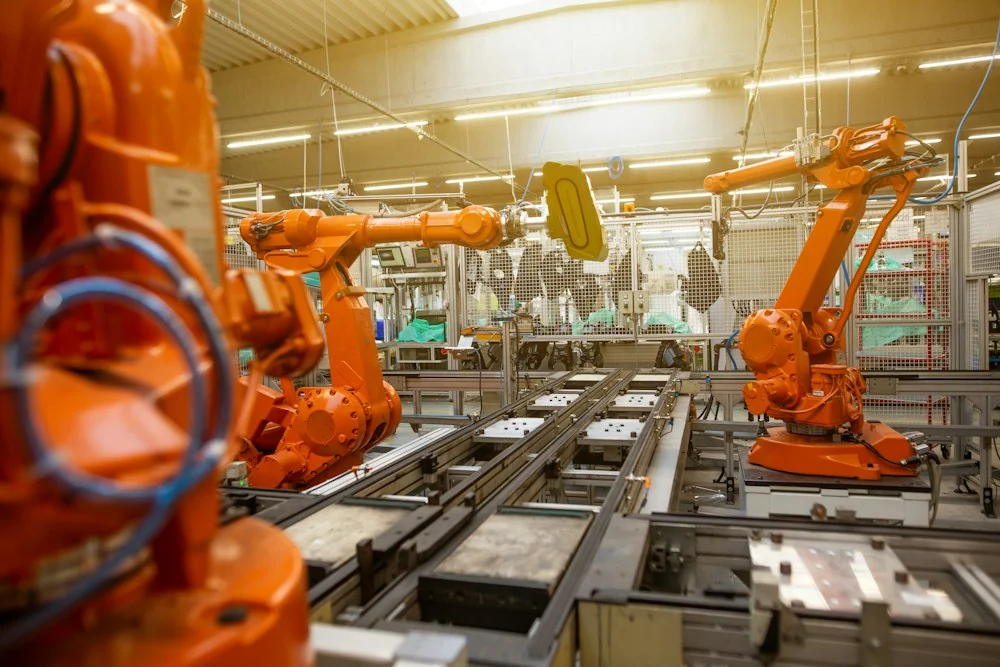
How is changeover verified across both part sizes, and where can operators check the active fixture and recipe?两种尺寸的工件如何验证换型?操作员在哪里核对当前夹具和配方?
If the network connection drops during production, how does the line record and reconcile inspection results for each part?如果生产中途断网,产线如何记录并补传每件产品的检测结果?
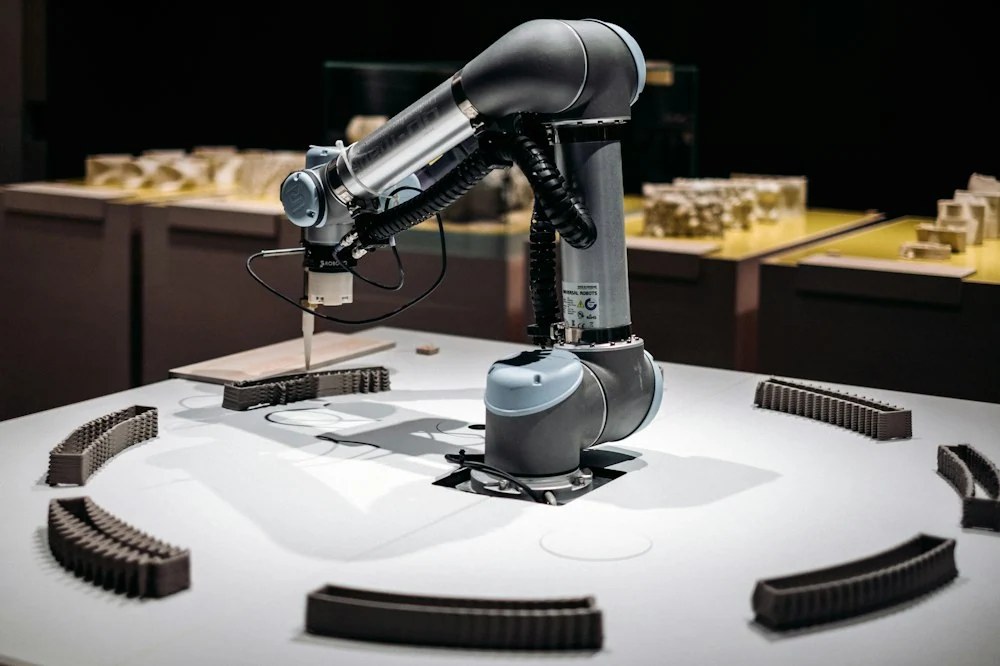
Which program backups are handed over, and can maintenance staff replace wear parts without dismantling adjacent equipment?设备交付时会移交哪些程序备份?更换易损件时是否需要拆卸相邻设备?
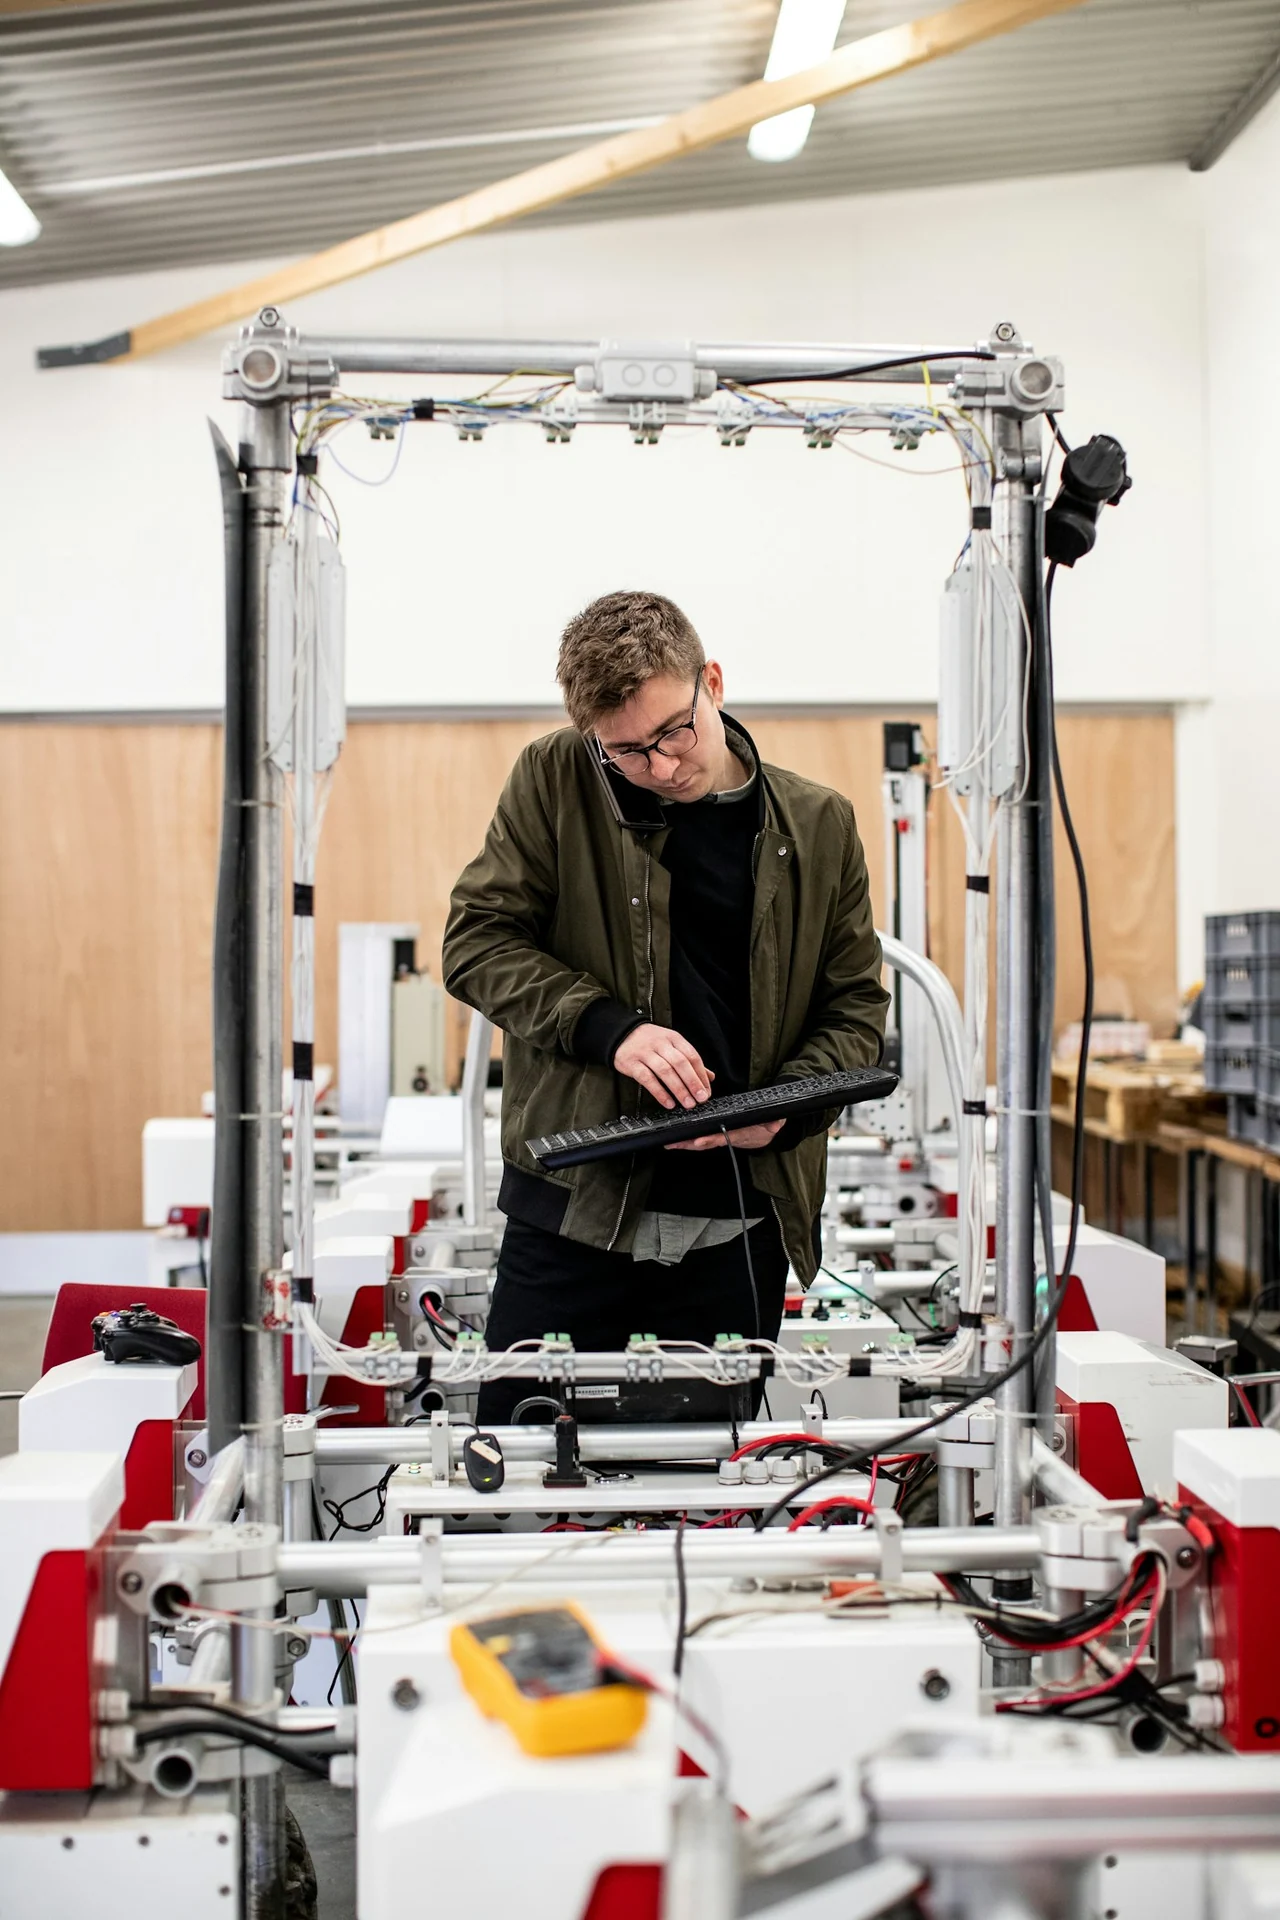
The quote depends on workpiece variation, required output, tooling, safeguarding, interfaces and installation scope. Compare proposals using the same acceptance conditions and scope.报价取决于工件差异、产出目标、工装、防护、接口及安装范围。对比方案时,应使用相同的验收条件和供货范围。
Sample readiness, drawing approval, lead times for selected components and the site's available installation window all affect the schedule.样件准备、图纸确认、选定部件的到货时间及现场可用安装窗口,都会影响交付周期。
Review controller models, firmware and available protocols. Agree which system owns each signal, what is recorded, and how the line operates during a network outage.先核对控制器型号、固件和可用协议,再明确各信号的归属、需记录的数据及断网时的运行方式。
Agree on part types, sampling, the test window and how planned stops are counted. Record defects and downtime alongside good output.事先约定产品型号、抽样方法、测试时段及计划停机的计入规则,并同时记录良品、不良与停机。
Train operators on starting, stopping, recipe changes and alarm escalation. Maintenance staff review inspection points, approved recovery procedures and backups.操作人员学习启停、换型和报警上报,维护人员熟悉点检项目、获准执行的恢复流程及备份。